

2 Industrial Extrusion Lines
Automated hydraulic extrusion presses powered by dual large-capacity billet heating furnaces, extruding 6063-T5 and 6063-T6 alloys to tight dimensional tolerances (EN 755 / ASTM B221 compliance).
"At Pak Alumex, our core commitment is to deliver structural reliability, dimensional accuracy, and weather-resistant surface finishes that exceed rigorous international engineering benchmarks."
Since our establishment, Pak Alumex Aluminium Industries has maintained a singularly focused operational philosophy: manufacturing heavy-duty, high-performance architectural profiles that empower architects, structural engineers, and commercial contractors worldwide.
By integrating automated billet heating, precision extrusion presses, computerized anodizing rectifiers, and automated electrostatic powder coating under a single QA protocol, we assure complete batch-to-batch consistency and zero mechanical defect tolerance.
Operating from a multi-acre industrial site on Painsra Road, Gojra, our plant combines melt furnaces, extrusion lines, surface treatment baths, and automated packing bays.
Automated hydraulic extrusion presses powered by dual large-capacity billet heating furnaces, extruding 6063-T5 and 6063-T6 alloys to tight dimensional tolerances (EN 755 / ASTM B221 compliance).
Equipped with chromate-free multi-stage pre-treatment wash tanks and automated spray booths, delivering 60–80 µm dry film builds certified for high UV and impact resistance.
Heavy-duty electro-chemical oxidation system generating controlled 10 to 25 micron anodic films in natural silver, champagne, bronze, and architectural black finishes.
Advanced heat-transfer vacuum system reproducing authentic timber grain finishes (Oak, Walnut, Teak) on durable, non-combustible powder-coated aluminium bases.
On-site die correction, wire EDM, and CNC milling facilities capable of translating custom DWG/DXF architectural sections into production-ready steel extrusion dies.
Dedicated staging bay with automated film wrapping, bundle strapping, and seaworthy wooden crating for direct export shipments via Karachi seaport.
A visual inspection of our extrusion halls, automated surface treatment lines, material handling systems, and quality control stations.
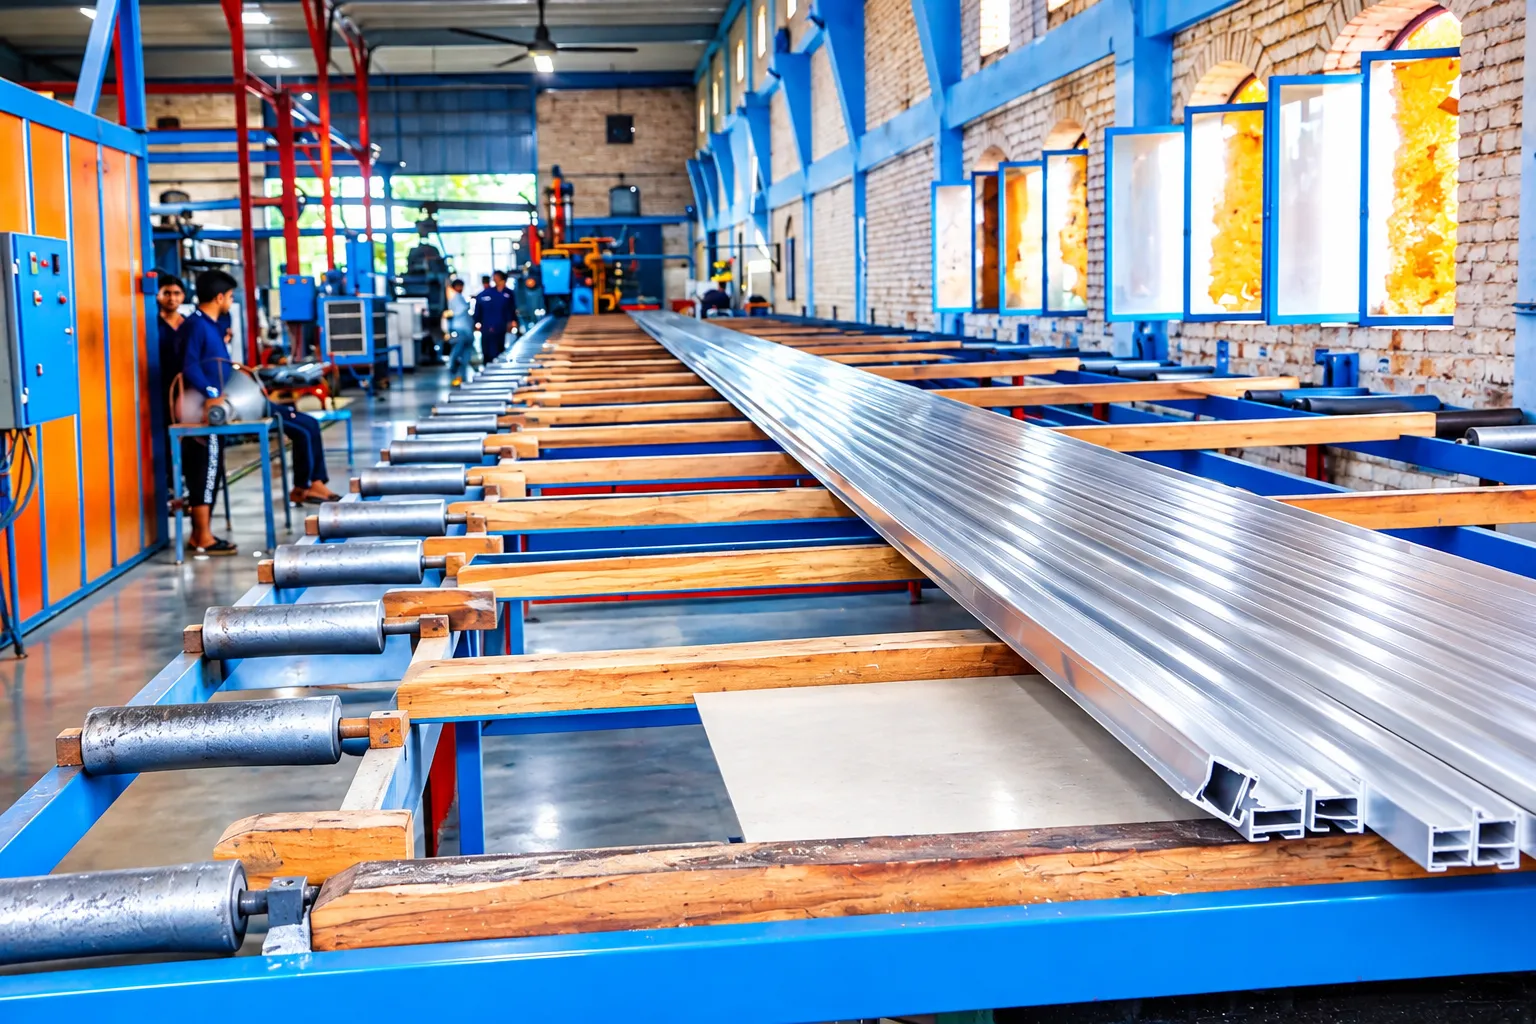
Automated run-out table and cooling beds handling hot extruded profile lengths.
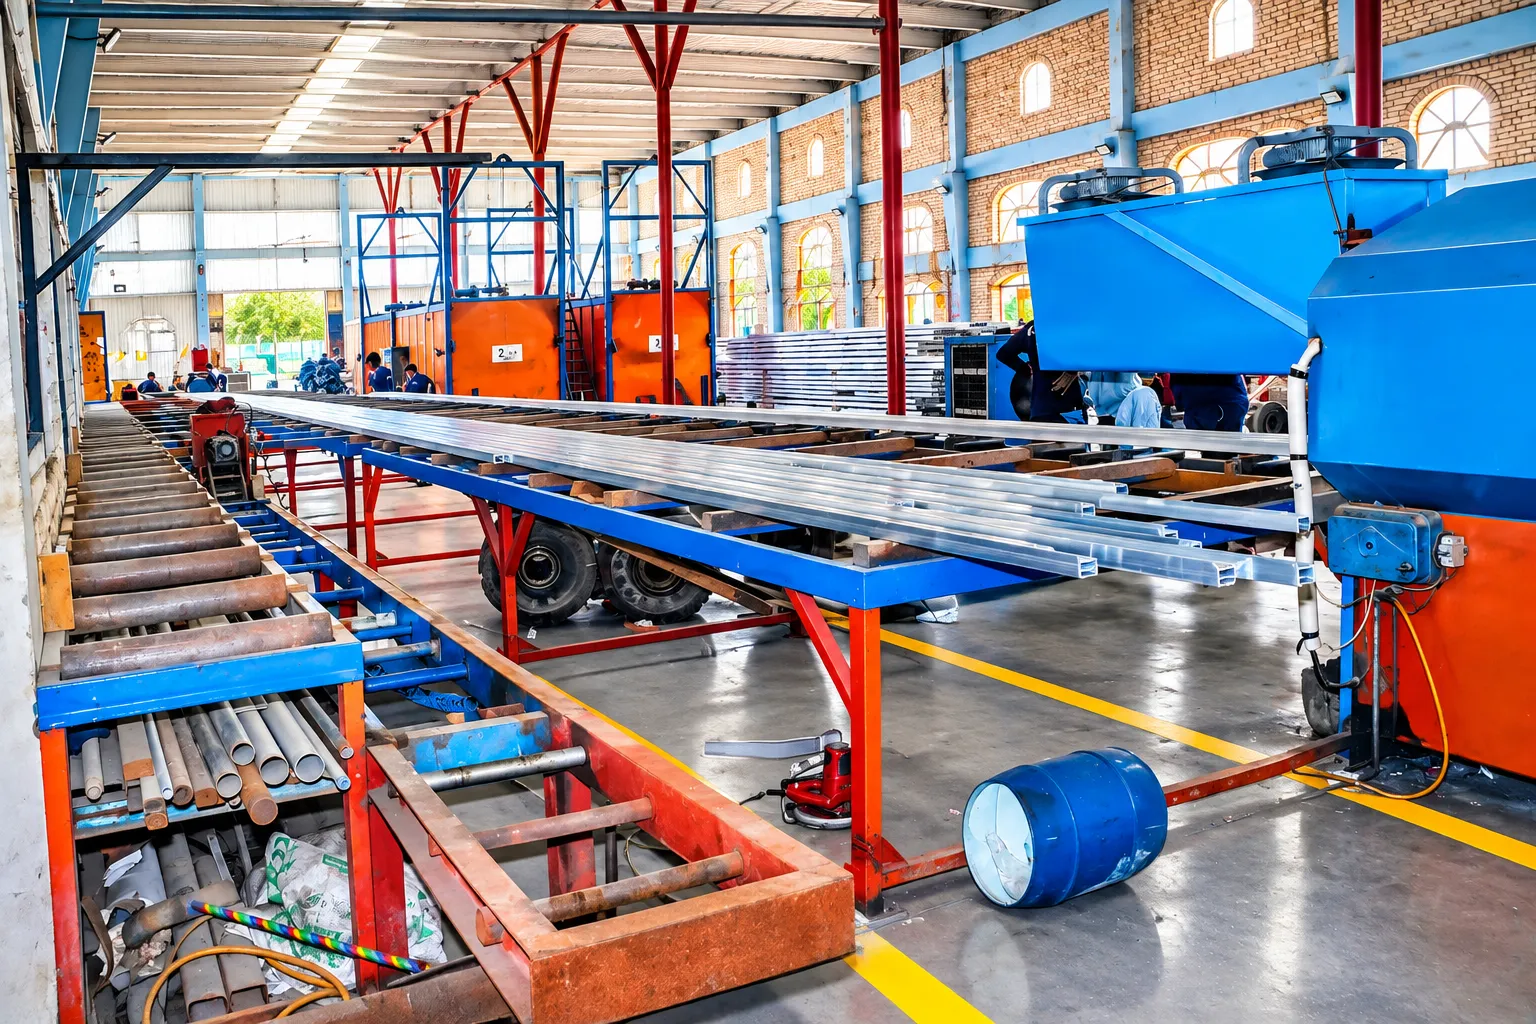
Systematic profile staging and age-hardening furnace transfer operations.
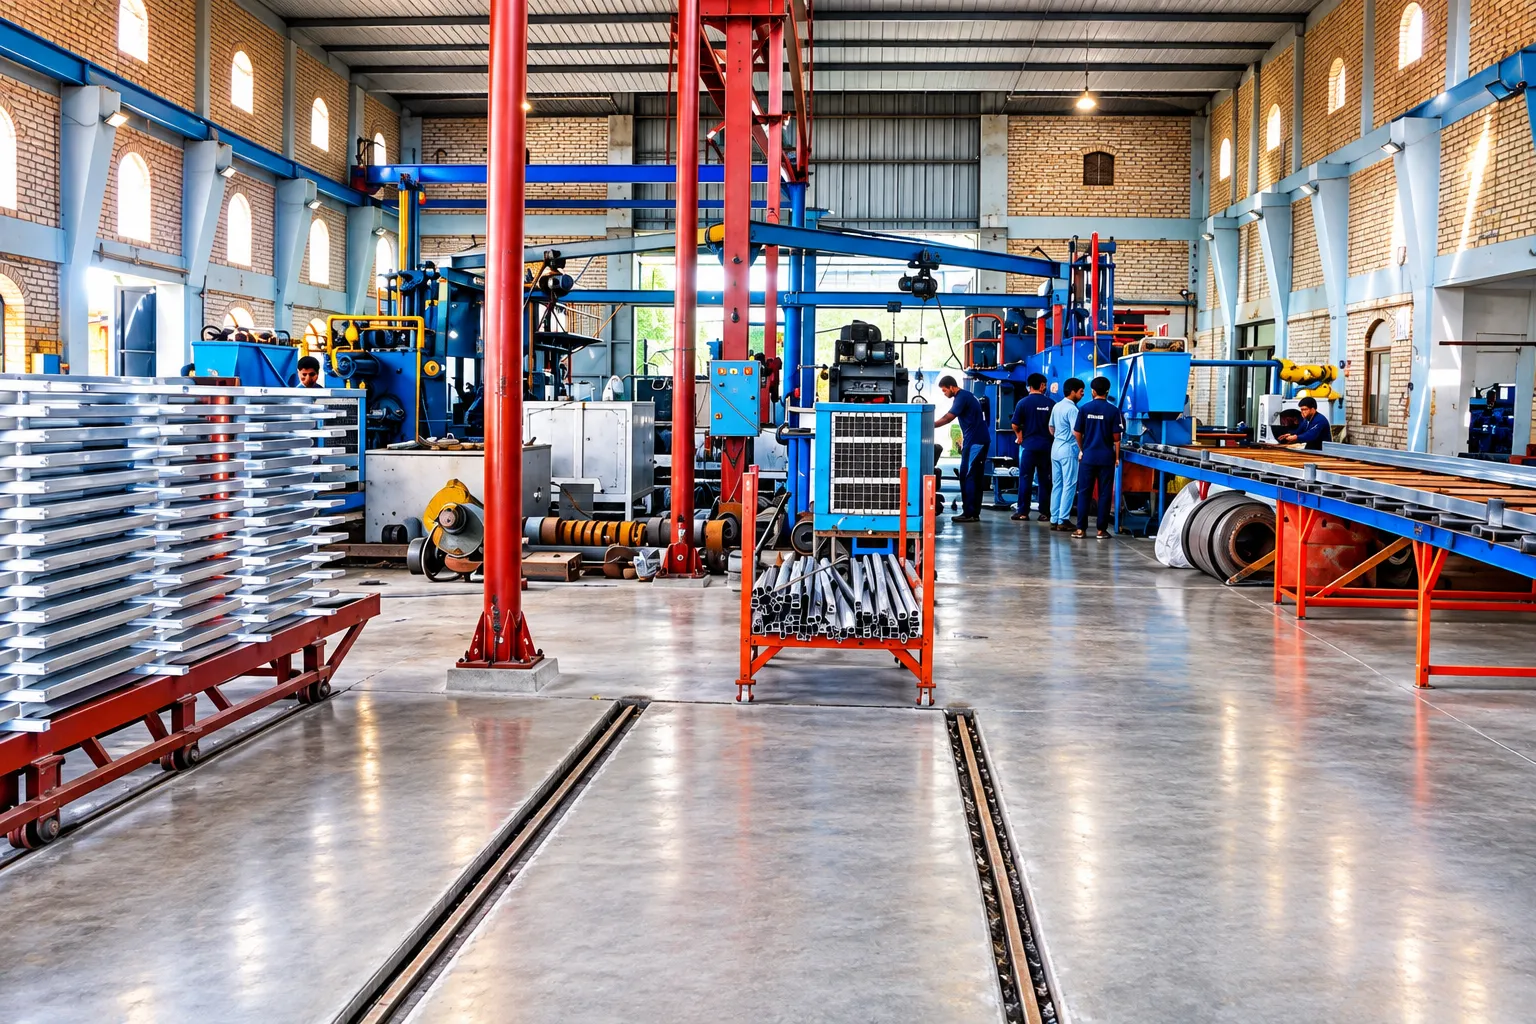
Aisle organization for extruded sections awaiting surface treatment.
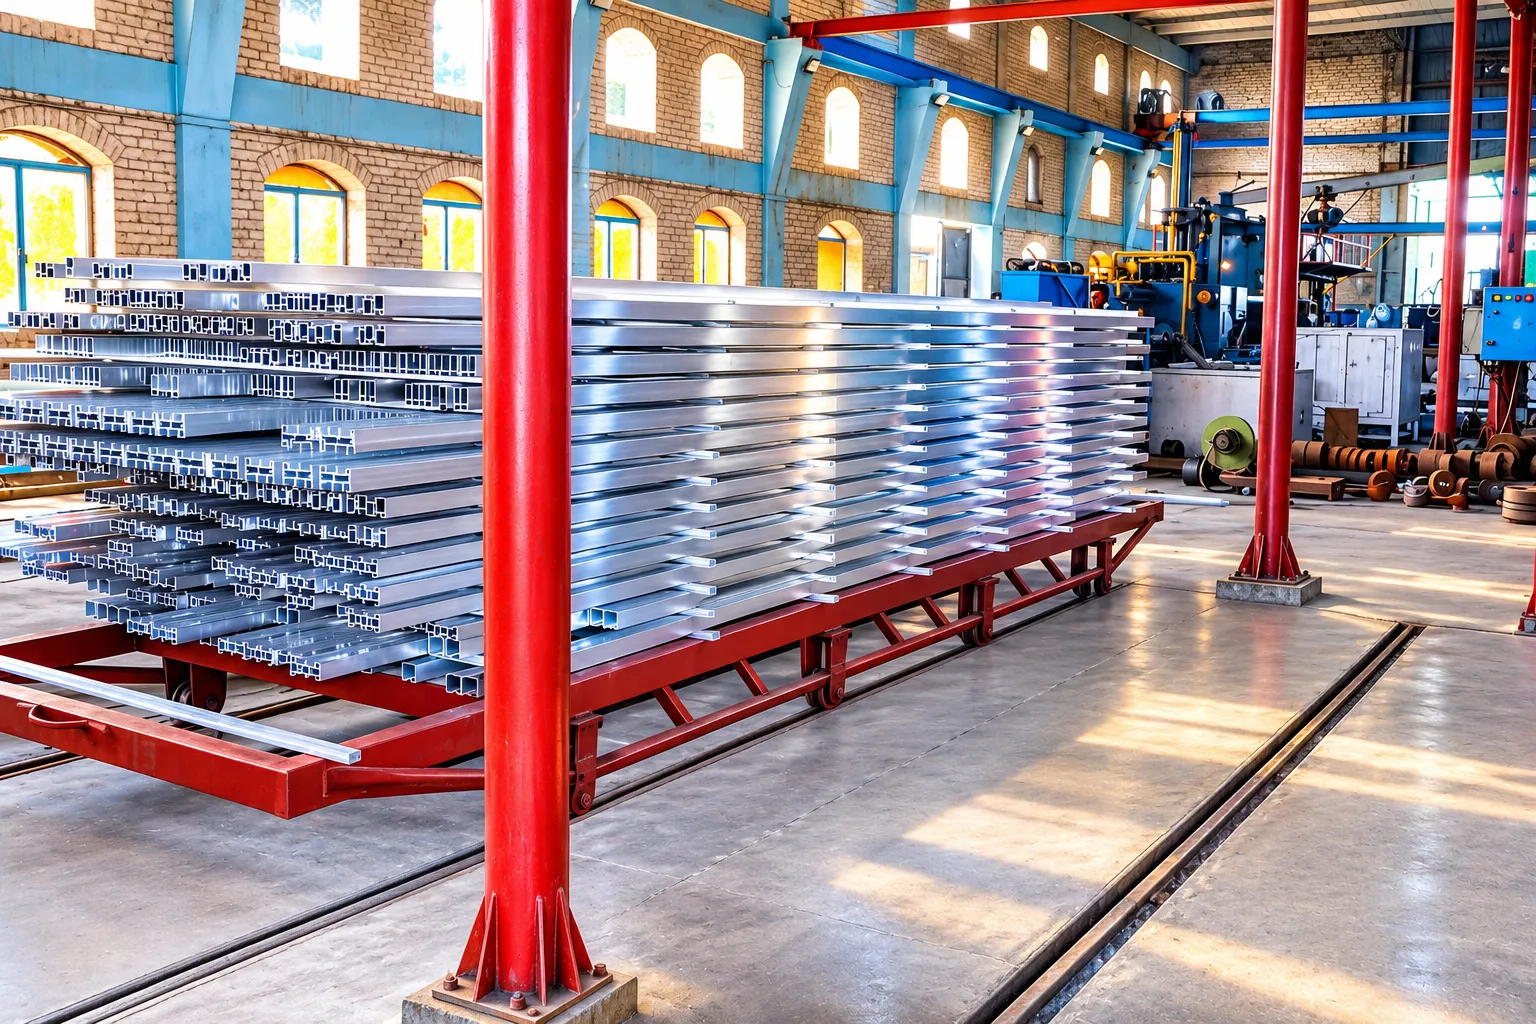
Quality-checked architectural lengths prepared for protective masking.
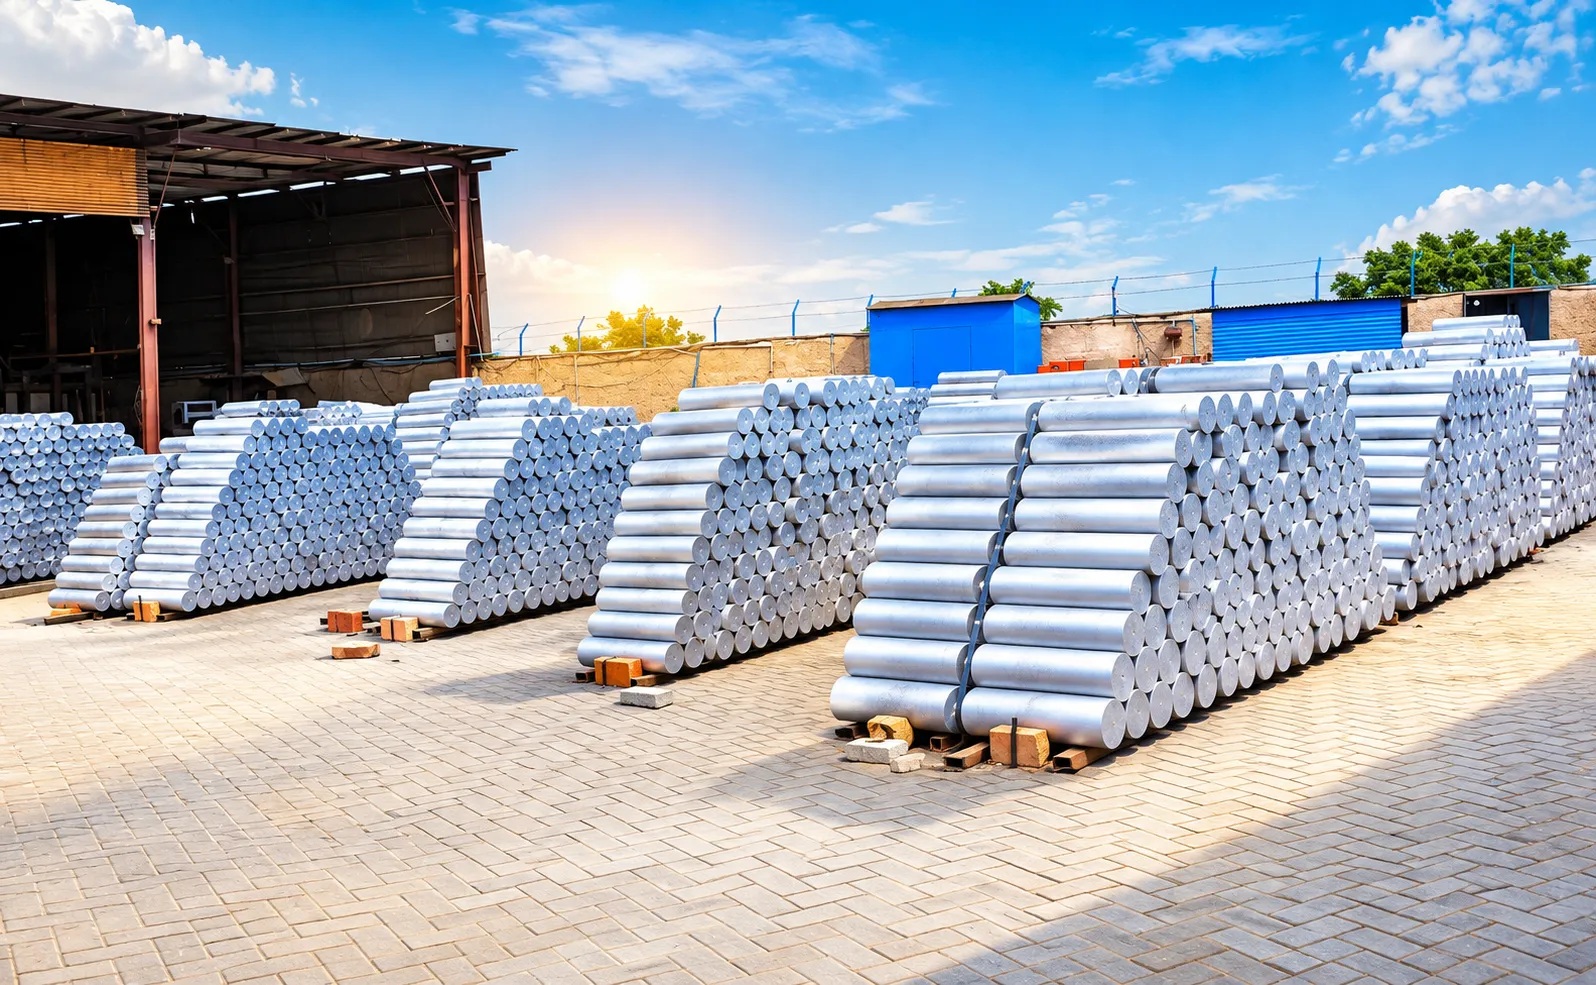
High-purity primary aluminium billets categorized by alloy and melt batch numbers.
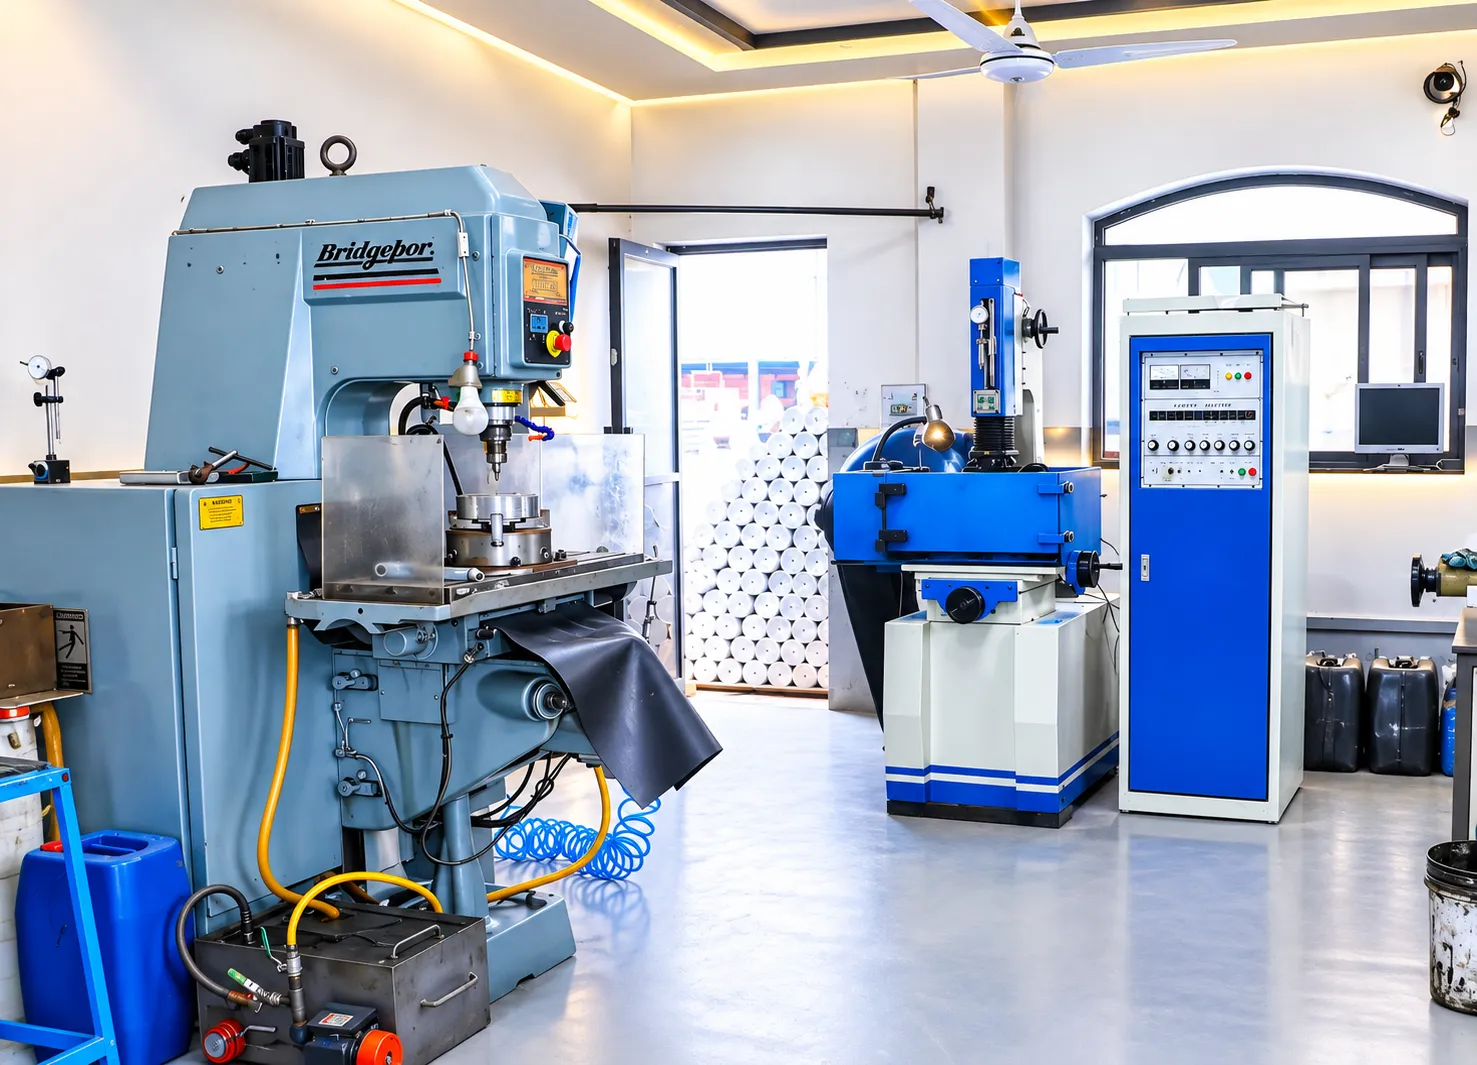
Precision milling and maintenance equipment for extrusion die geometry.
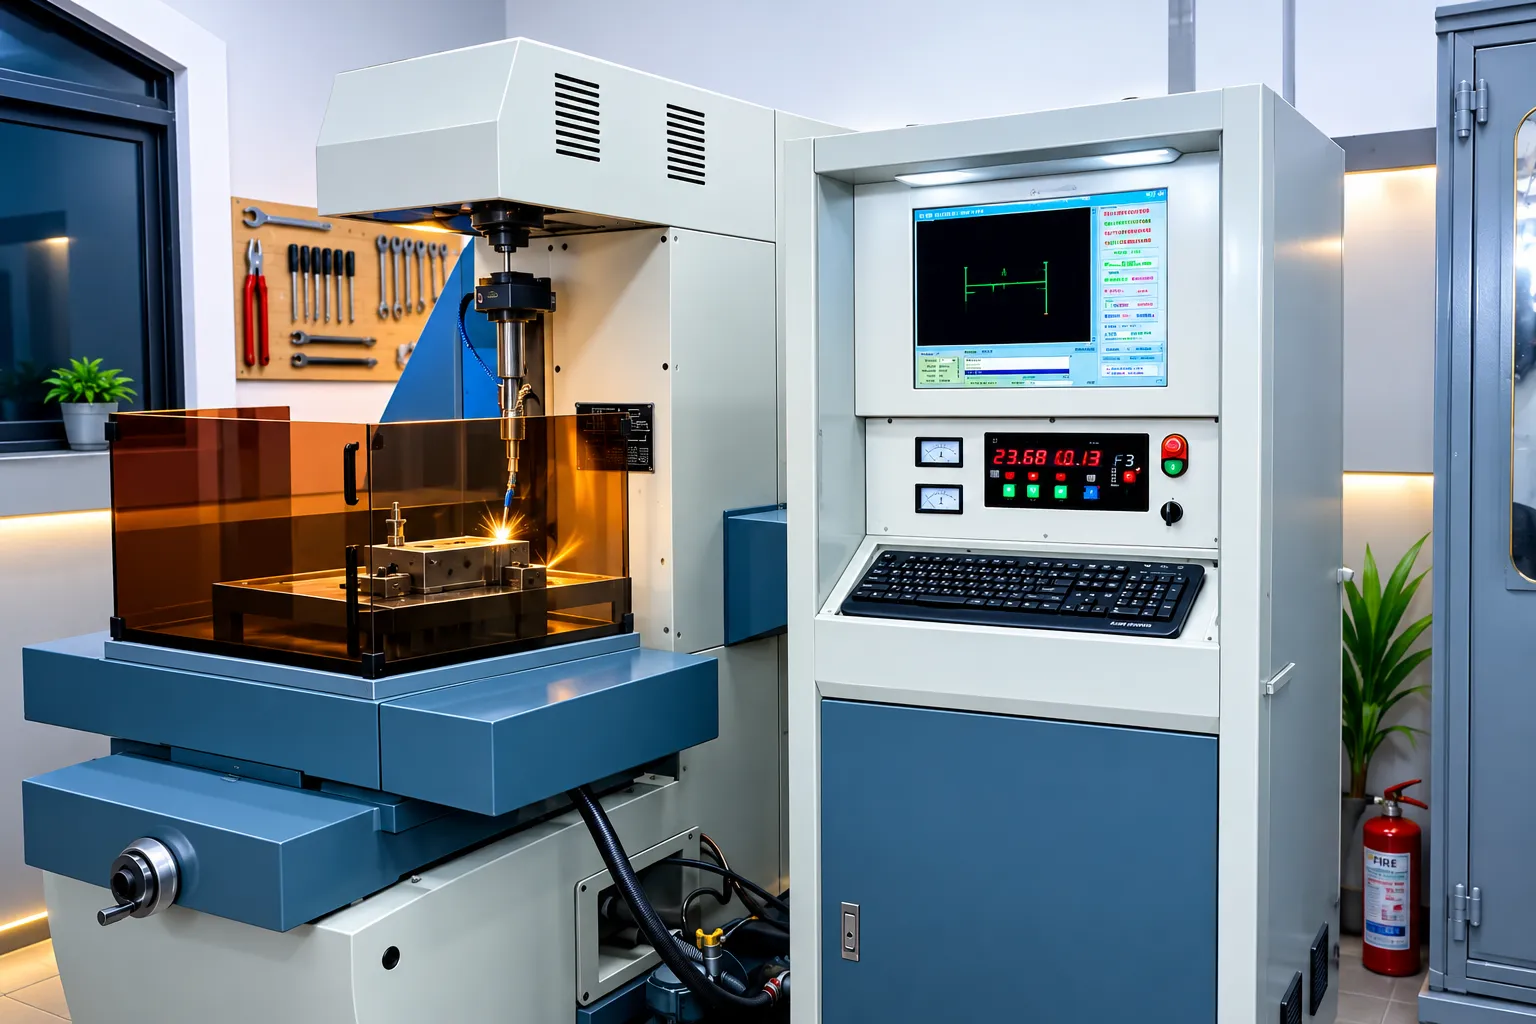
Automated profile drilling, slotting, and corner cleat notch machining.
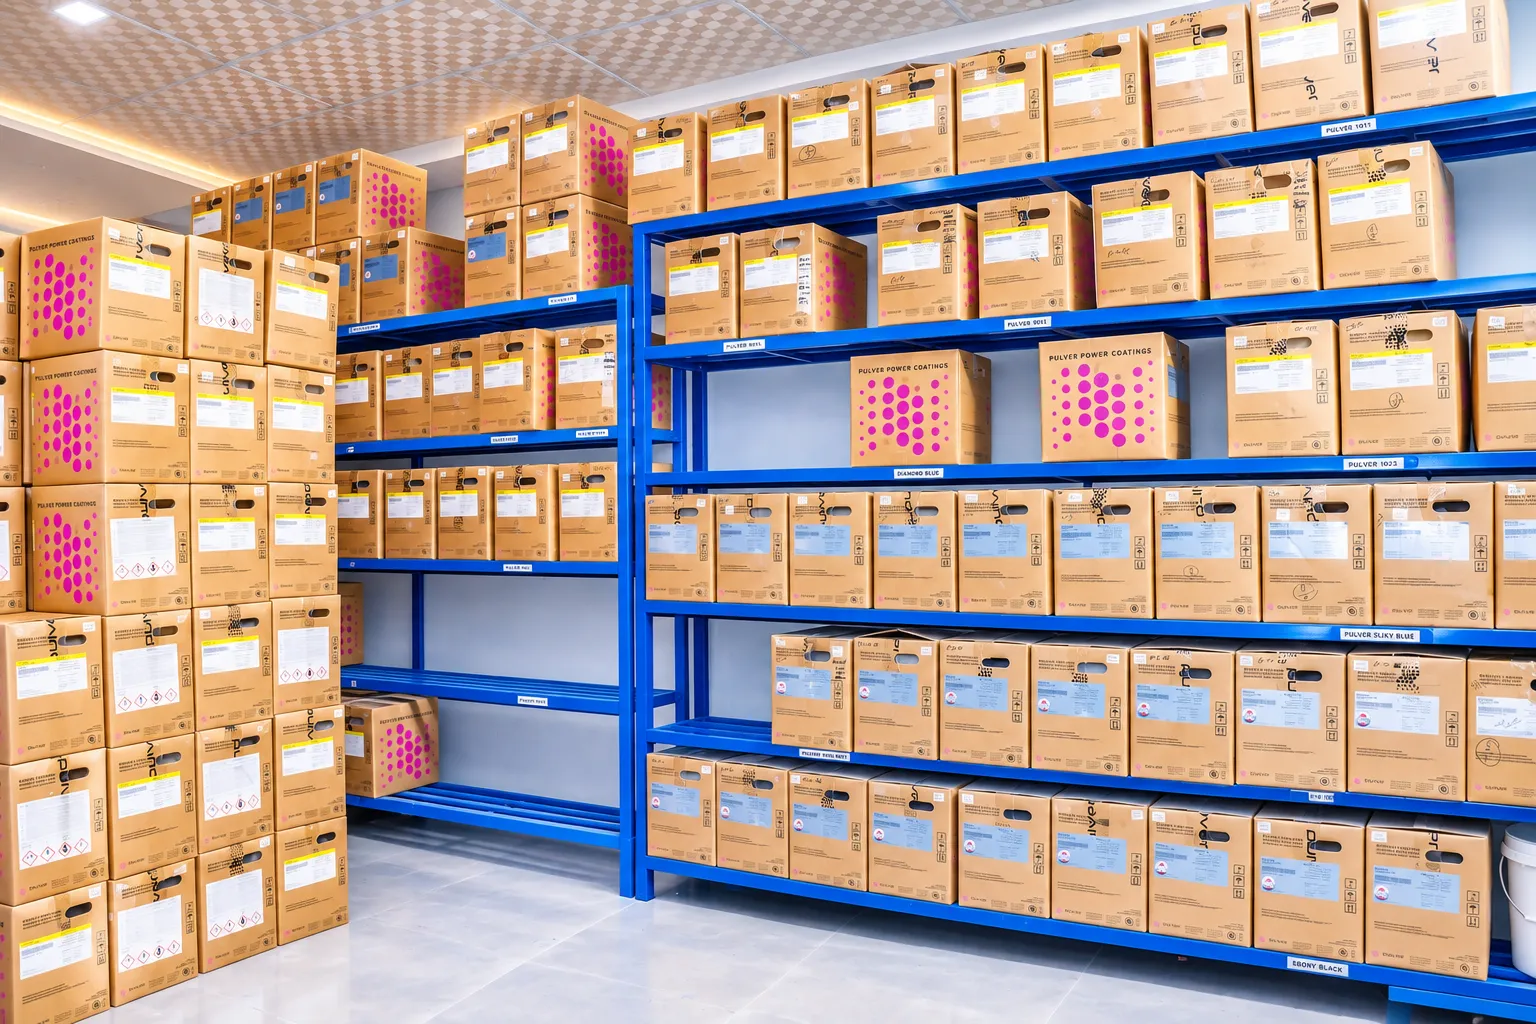
Temperature-controlled storage for Qualicoat-approved architectural powders.
Every order manufactured at Pak Alumex passes through mandatory inspection stages to verify chemical composition, web-to-flange dimensional tolerances, mechanical temper, and surface coating adhesion.
Incoming primary aluminium billets are spectro-analyzed prior to heating to guarantee precise Magnesium and Silicon ratios within AA6063 parameters.
Powder coatings are tested via magnetic film thickness gauges (60–80 µm) and cross-hatch tape-adhesion tests (ISO 2409) to confirm film bonding.
Extrusions are checked against laser micrometers and master CAD templates to guarantee structural fitment for curtain wall mullions and window sashes.
Provide your section drawings, profile specifications, or project bill of quantities. Our technical sales engineering department provides prompt feasibility analysis, weight schedules, and competitive export quotations.