

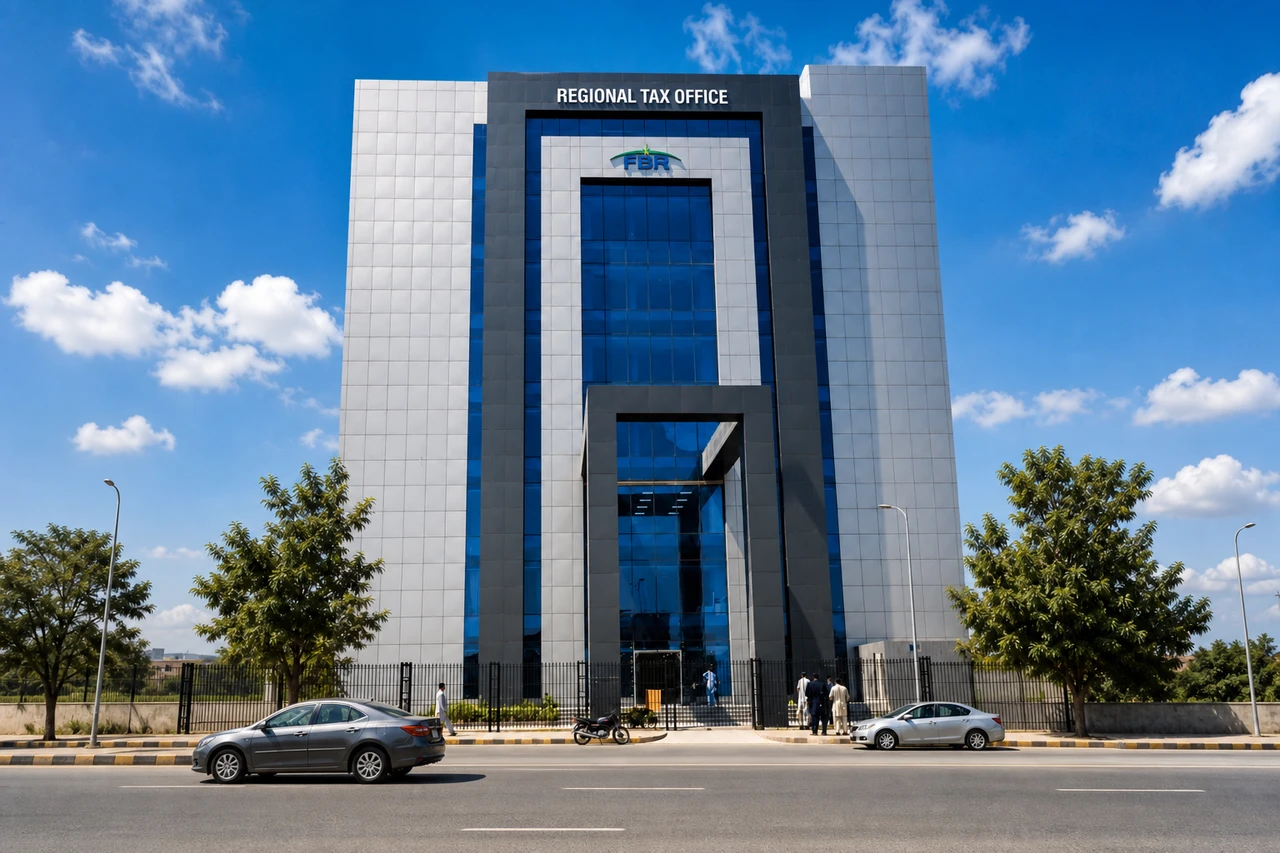
Main Elevation Glazing
Vertical mullions engineered for wind resistance and thermal movement.
The FBR Regional Tax Office in Sector G-9, Islamabad, stands as a major public commercial headquarters requiring long-term structural integrity, strict thermal insulation standards, and high-durability weather protection.
Pak Alumex Aluminium Industries manufactured and supplied precision 6063-T6 architectural aluminium extrusions and Qualicoat-compliant exterior powder coating for the entire envelope. Our direct engineering support ensured seamless alignment between die geometry, wind-load capacity, and site assembly by regional fabrication partners.
For international procurement teams, architects, and facade consultants, our supply parameters reflect strict compliance with global architectural standards.
| Parameter | Engineering Standard / Value | Technical Advantage for Overseas Buyers |
|---|---|---|
| Extrusion Billet Quality | A-Grade Primary Aluminium Billet (6063 Alloy) | Ensures uniform mechanical strength, superior surface finish, and elimination of structural inclusions. |
| Temper Specification | T6 Artificial Ageing Treatment | Delivers higher ultimate tensile strength and yield stress required for large-span curtain wall mullions. |
| Coating Film Build | 60–80 microns (Polyester Architectural Powder) | Provides continuous barrier protection against UV degradation, chalking, and urban atmospheric pollution. |
| Pre-treatment Chemistry | Chromate-free conversion coating process | Complies with modern environmental safety rules while assuring long-term adhesion performance. |
| Profile Wall Thickness | 1.8 mm – 3.0 mm structural wall zones | Calculated specifically for high wind load pressure without unnecessary profile mass or material waste. |
| Glazing Compatibility | 24 mm – 28 mm Double Insulated Glass Units (IGU) | Optimized thermal insulation coefficient (U-value) for energy-efficient commercial interior climate control. |
International facade projects demand consistent lot-to-lot tolerances and single-source quality control. Pak Alumex manages every stage of production under one roof.
Extruded using advanced automated presses with real-time temperature control. Profiles are checked against critical DXF drawing tolerances before advancing to artificial ageing ovens.
Before coating, all profiles undergo rigorous degreasing, acid etching, and chromate-free passivation baths to eliminate oxidation and establish key anchor chemistry for the powder coating layer.
Finished lengths undergo cross-hatch adhesion, impact, and film thickness gauge checks. Profiles are individually wrapped in protective PE film and bundle-strapped for overseas ocean shipping.
Examine the crisp sightlines, uniform color consistency, and structural execution delivered across multi-story commercial glazing installations.
Vertical mullions engineered for wind resistance and thermal movement.
Integrated casement sashes with continuous EPDM weather gaskets.
Bespoke section geometries produced for complex architectural reveals.
High-durability powder-coated frame assembly built for long service life.
Key answers regarding custom dies, quality compliance, alloy verification, and global dispatch.
Every raw billet batch undergoes optical emission spectrometry to verify 6063 alloy chemical limits. Post-extrusion, artificial ageing in controlled ovens brings the profiles to T5 or T6 temper, verified using Webster and Webster/Brinell hardness testers before coating or dispatch.
Yes. We develop project-specific extrusion dies from CAD DWG/DXF drawings. Our tooling engineers evaluate wall thickness ratios, press pressure requirements, and dimensional tolerances. First-article samples are extruded and dimensionally verified before bulk production approval.
Extrusions are protected with non-staining surface protective film, interleaved with foam sheeting, and tightly strapped into seaworthy wooden crates or heavy-duty bundle wraps designed to withstand transshipment handling and ocean freight vibration.
All export consignments include Mill Test Certificates (MTC), Coating Inspection Reports (dry film thickness and adhesion test logs), Commercial Invoices, Packing Lists, Bill of Lading, and Country of Origin Certificates.
Planning a commercial facade or seeking custom aluminium profile extrusions? Download our complete engineering catalog and system technical sheets.